




2014
Establish a comprehensive new materials enterprise integrating R&D, production, and import-export trade.
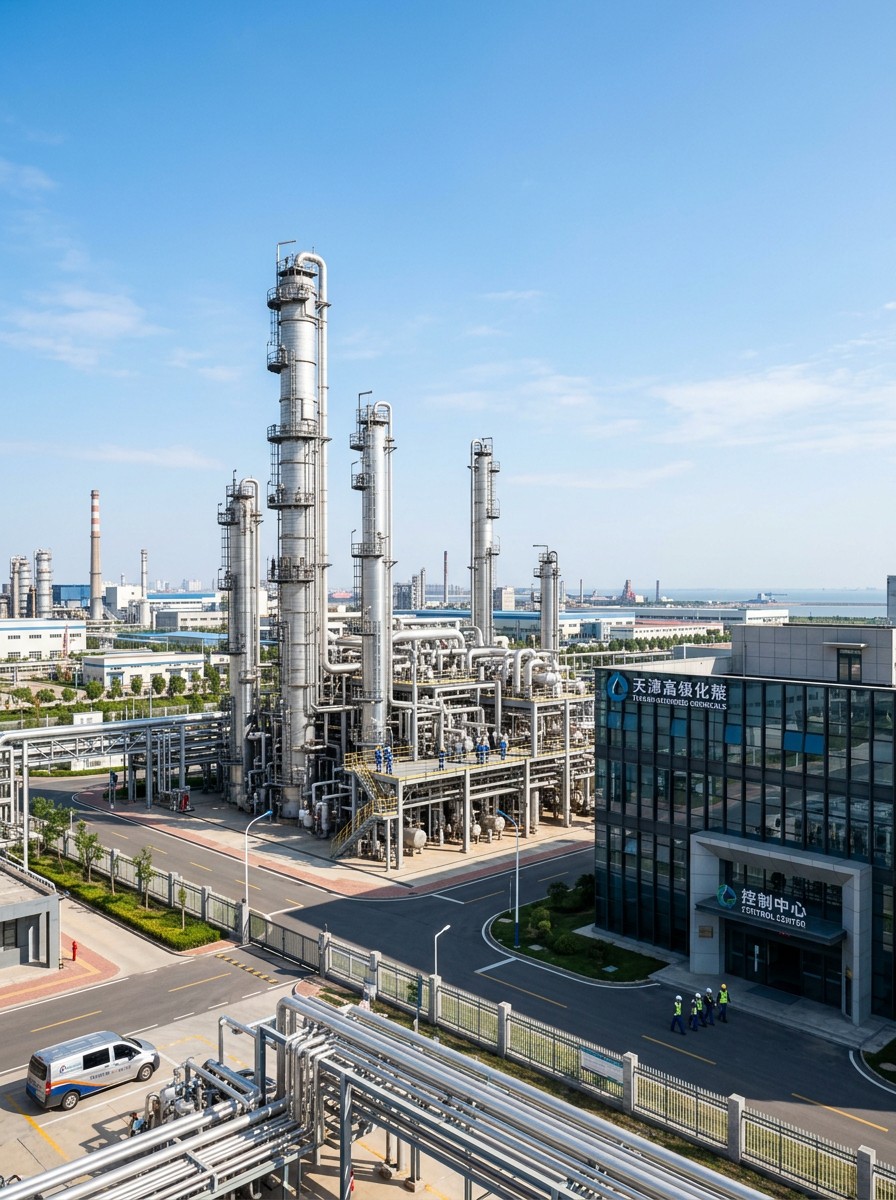
Wanhua Chemical Shandong Co., Ltd. has built solid expertise through years of dedicated efforts in the chemical industry, with an annual export volume of 5 million tons. Our product portfolio covers ten major categories including new energy & new materials, chemical fertilizers, organic amines, acetic acid and its derivatives, polyols, synthetic resins, polyurethanes, flavors and fragrances, additives & catalysts, and inorganic chemicals, totaling over 100 varieties.
Chemical Polymers
We have successively obtained certifications for ISO9001 Quality Management System, ISO14001 Environmental Management System, OHSAS18001 Occupational Health and Safety Management System, as well as ISO50001 Energy Management System. Our intrinsic safety performance, environmental protection standards and carbon utilization rate rank among the industry leaders. For eight consecutive years, we have been recognized as an outstanding energy-saving enterprise in the coal-to-ammonia, coal-to-methanol and coal-to-acetic acid sectors. Our asset quality, investment efficiency, operational efficiency and labor productivity have always stayed at the forefront of the industry.
How We Work
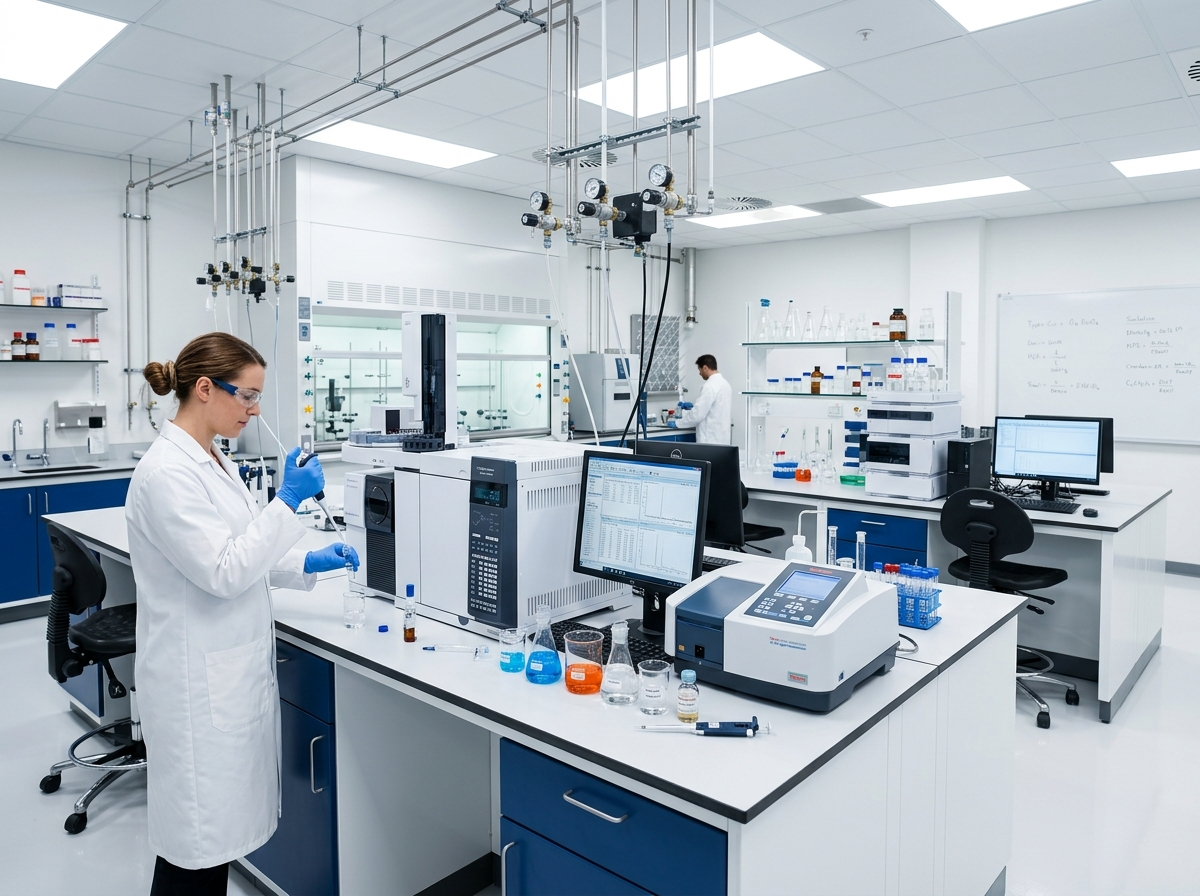
Rigorous incoming raw material quality assessment. Every batch of feedstock undergoes thorough gas chromatography (GC-MS), high-performance liquid chromatography (HPLC), and spectrophotometric analysis to guarantee 99.8%+ baseline purity prior to reaction initiation.
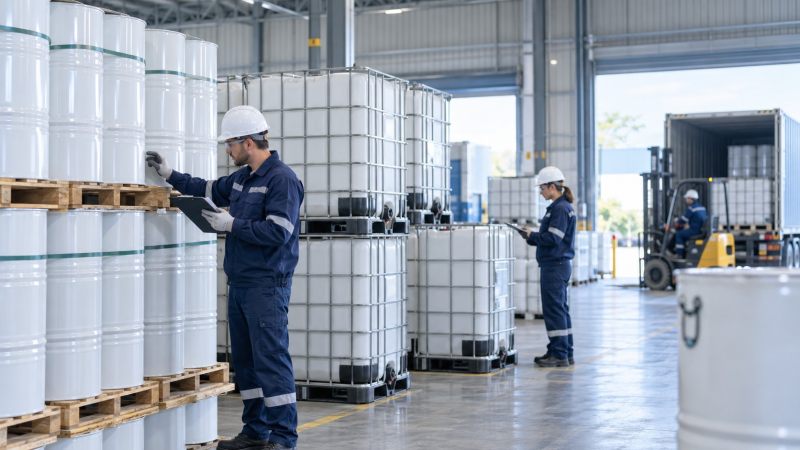
Complete supply chain transparency with traceable batch archiving, ensuring every drum and ISO tank matches certified export specifications and strict customer tolerances.
Continuous flow chemical synthesis coupled with multi-stage fractional distillation columns. We precisely regulate temperature, pressure, and catalyst ratios to minimize thermal degradation and suppress isomer formation.
Automated DCS control loops continuously monitor critical reaction parameters 24/7, guaranteeing dependable batch-to-batch repeatability and ultra-low impurity profiles.
Standardized UN-rated packaging including 200L galvanized steel drums, 1000L IBC totes, and ISO tank containers. Packed under dry nitrogen blanketing to prevent moisture absorption and oxidation.
Full global trade documentation provided with every shipment: REACH compliance certificate, GHS-standard SDS, Certificate of Analysis (COA), and seamless international customs logistics support.
Our Journey of Growth
R&D Center
We attach great importance to technological innovation and have built a professional R&D team composed of senior engineers and technical personnel. Equipped with an independent laboratory and advanced testing equipment, we carry out continuous product research, development and optimization. We also maintain long-term cooperation with well-known universities and research institutes, constantly improving our customization capacity and technological level, to provide personalized chemical solutions for global customers.
Quick Chemical RFQ Inquiry
Tell us your target specifications & our export team will respond within 24 hours.